Hollow heavy forgings
Shell Section Forging and Production
Heavy open die presses, manipulators and tooling to forge seamless shells for pressure vessels and power plants.
Shell section forging makes large, seamless hollow cylinders from solid ingots. These shells are used in pressure vessels, nuclear reactors, steam generators, hydro-processing reactors and wind towers. A seamless forged shell has no longitudinal weld, which improves strength and reduces inspection work.
Hind Presses & Automation supplies the heavy open die forging presses, manipulators and tooling needed for shell section production, up to the 22000 ton open die forging press.
Key features
Seamless shells
Hollow cylinders forged without longitudinal welds.
Heavy press capacity
Force and daylight for large ingots and hollow parts.
Mandrel tooling
Mandrels and saddles for drawing and expanding shells.
Heavy manipulator
Manipulators to handle hollow parts with precision.
Process support
Help with forging sequence planning for each shell size.
Quality focus
Even reduction for uniform structure through the wall.
Steps in shell section forging
The ingot is first upset to shorten and widen it. A punch then pierces the centre to make a hollow. The hollow is drawn out on a mandrel to lengthen it and reduce wall thickness. Finally, it is expanded on a saddle (mandrel ring forging) to reach the final diameter. Each step needs heavy force and accurate handling.
Specifications
| Process | Upsetting, piercing, mandrel drawing, saddle (ring) expansion |
|---|---|
| Press | Heavy open die forging press, up to 22,000 ton |
| Manipulator | Heavy railbound manipulator |
| Tooling | Punches, mandrels, saddles and supports |
| Materials | Low-alloy pressure vessel steels, stainless and special steels |
| Typical parts | Pressure vessel shells, reactor shells, steam generator shells, tower flanges |
| Support | Process planning, installation, training and service |
What you get
- Press and manipulator sizing
- Mandrel and saddle tooling
- Forging sequence planning support
- Integrated control system
- Installation and commissioning
- Operator training
- Spares and service support
Why forge seamless shells
A rolled and welded shell has a long weld seam that must be inspected and can be a weak point. A forged seamless shell has a uniform structure and no longitudinal weld, which is why it is preferred for high-pressure and nuclear service.
Equipment for shell section forging
Shell work needs a heavy press with large daylight, a strong manipulator and the right tooling. See our open die forging press and manipulator lines and the 300 ton forging manipulator.
Frequently asked questions
What is shell section forging?
It is the open die forging of large seamless hollow cylinders, used in pressure vessels, reactors and power plants.
What steps are used?
Upsetting, piercing, mandrel drawing and saddle (ring) expansion.
Why are forged shells better than welded shells?
They have no longitudinal weld and a more uniform structure, which suits high-pressure service.
What press size is needed?
It depends on shell size and weight. Large shells usually need presses of 10,000 ton and above.
What is the price of a shell section production line?
It depends on press, manipulator and tooling scope. Share your shell sizes for a quotation.
Which industries use forged shell sections?
Nuclear power, refineries and hydro-processing, steam generation, chemical plants and wind energy.
Can you supply the tooling as well?
Yes. Punches, mandrels, saddles and supports can be supplied with the press and manipulator.
More open die forging equipment
- 2500 Ton Double Column Fast Forging Press
- 5160 Ton Fast Forging Press
- 10000 Ton Open Die Forging Press
- 13500 Ton Fast Forging Press
- 22000 Ton Open Die Forging Press
- 300 Ton Forging Manipulator
- Open Die Forging Press and Manipulator
- Open die forging presses (800-22,000 ton)
Not sure which machine fits your part? Talk to our engineers or call +91-96541 87777.
Watch the press in action
Other presses we supply
SMC and Composite Hydraulic Presses
Compression moulding presses for SMC, BMC and composite components.
View details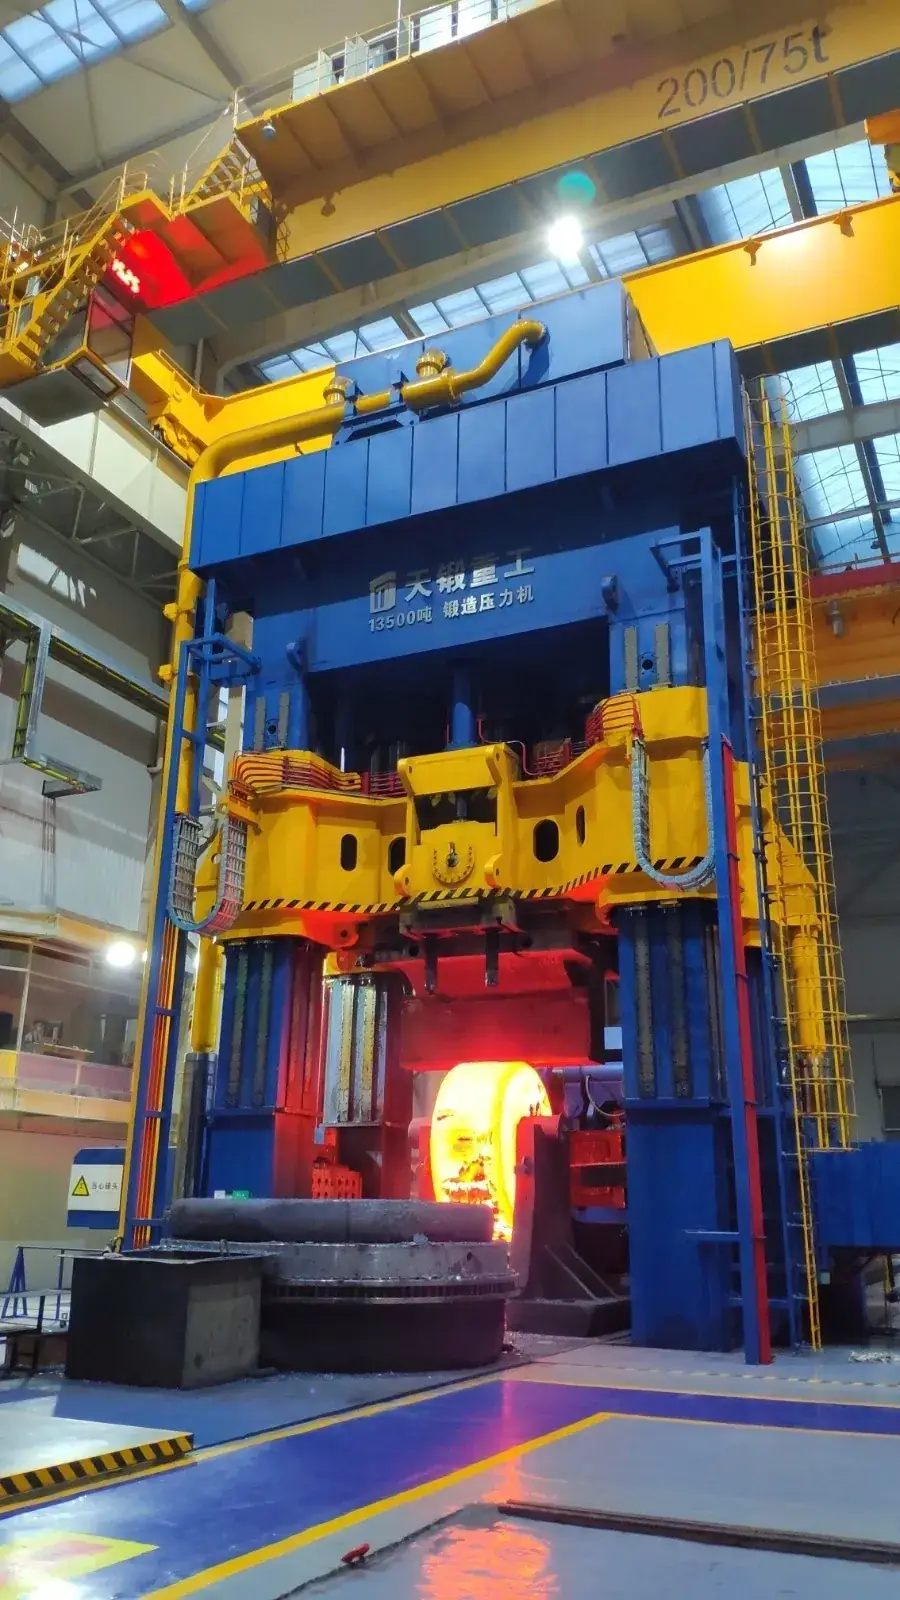
Open Die Forging Hydraulic Presses
Open die forging hydraulic presses from 800 to 22,000 ton with manipulators and automation.
View details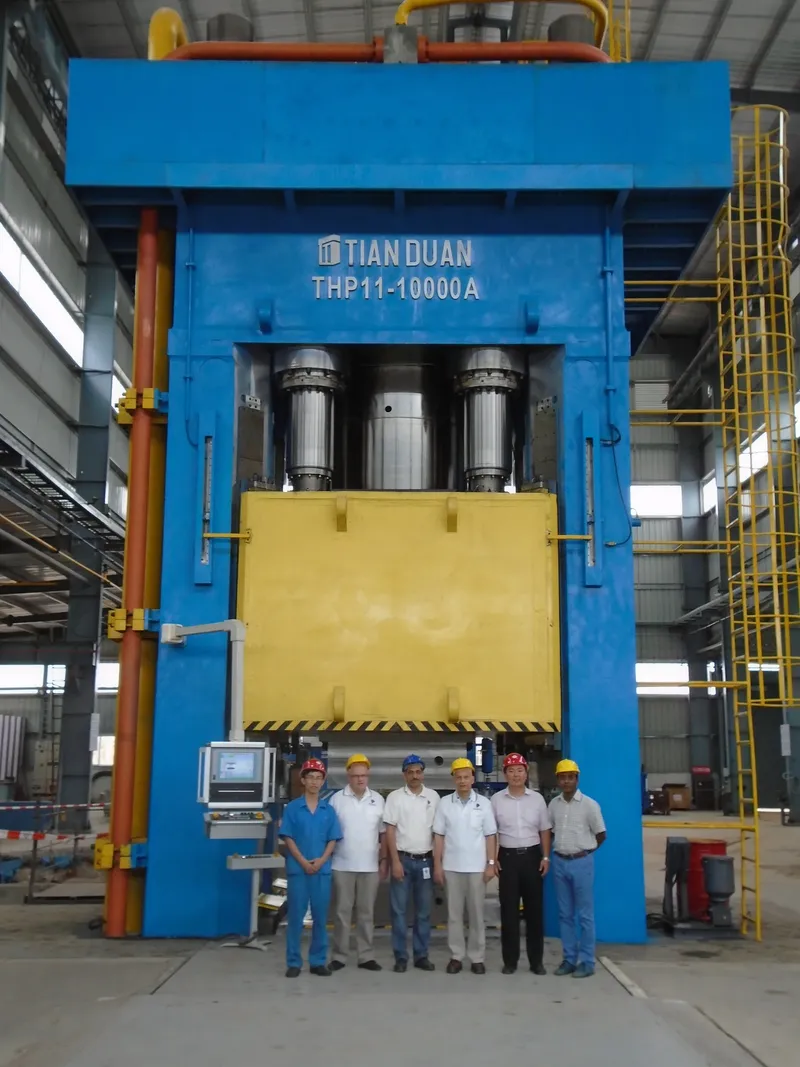
Close Die Hydraulic Forging
Precision close die forging presses for repeatable near-net-shape parts.
View details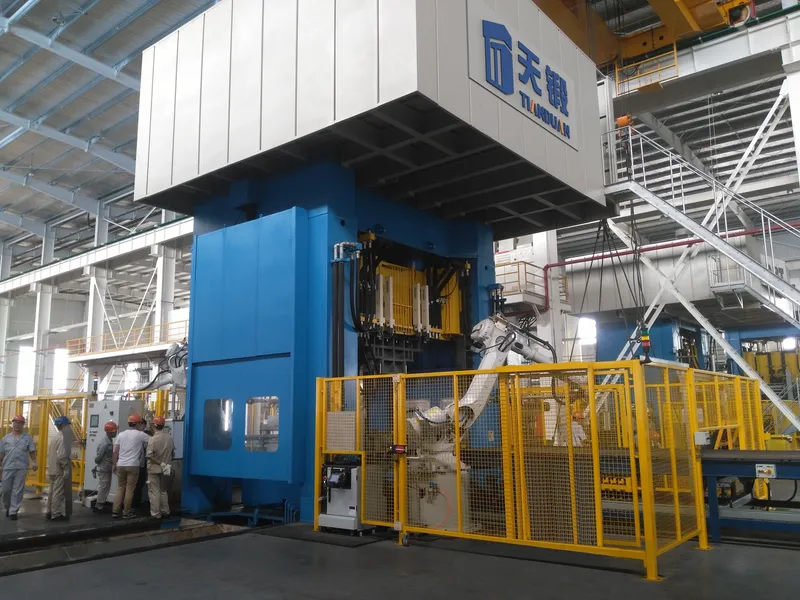
Hot Stamping Hydraulic Presses
Press hardening presses for ultra high strength automotive parts.
View details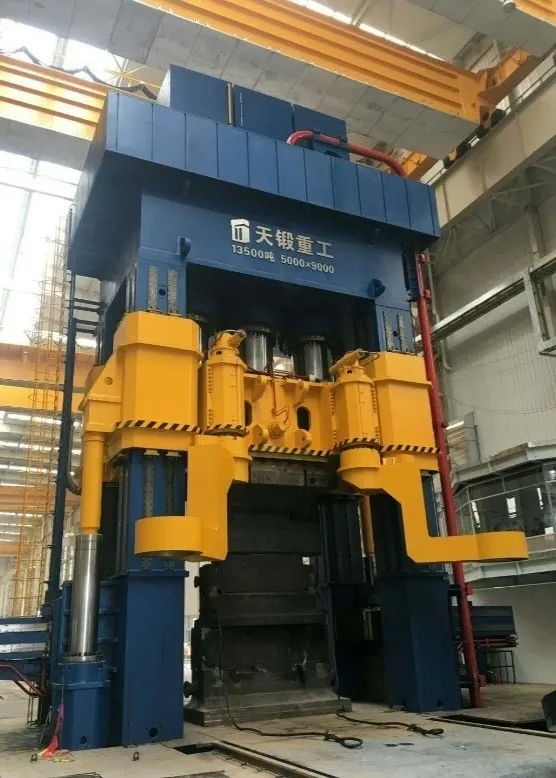
Ring Blank Hydraulic Forging Press
Ring blank forging presses, including 5,000 ton ring forging presses.
View details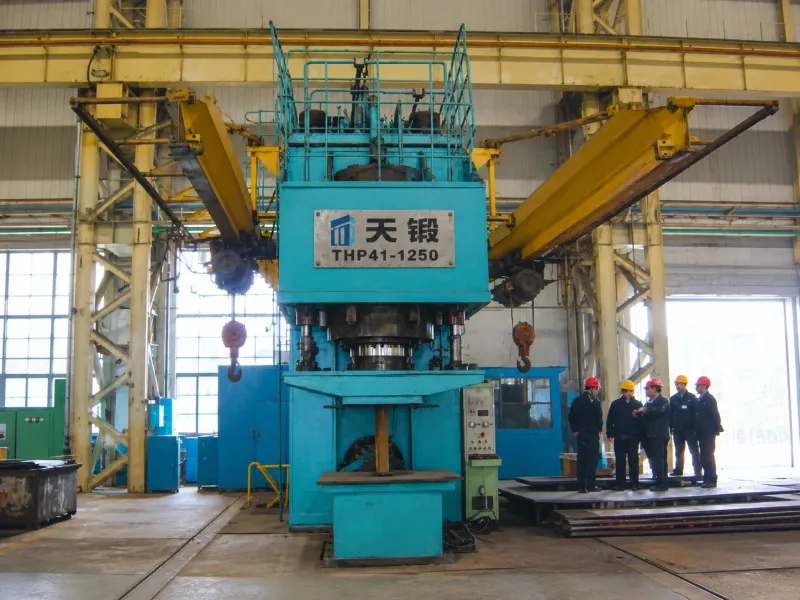
Ship Building Hydraulic Presses
Plate bending, forming and flanging presses for shipyards.
View detailsTell us your requirement. An engineer will reply on WhatsApp.
Share tonnage, material, part size and annual output for a fast, accurate quotation.